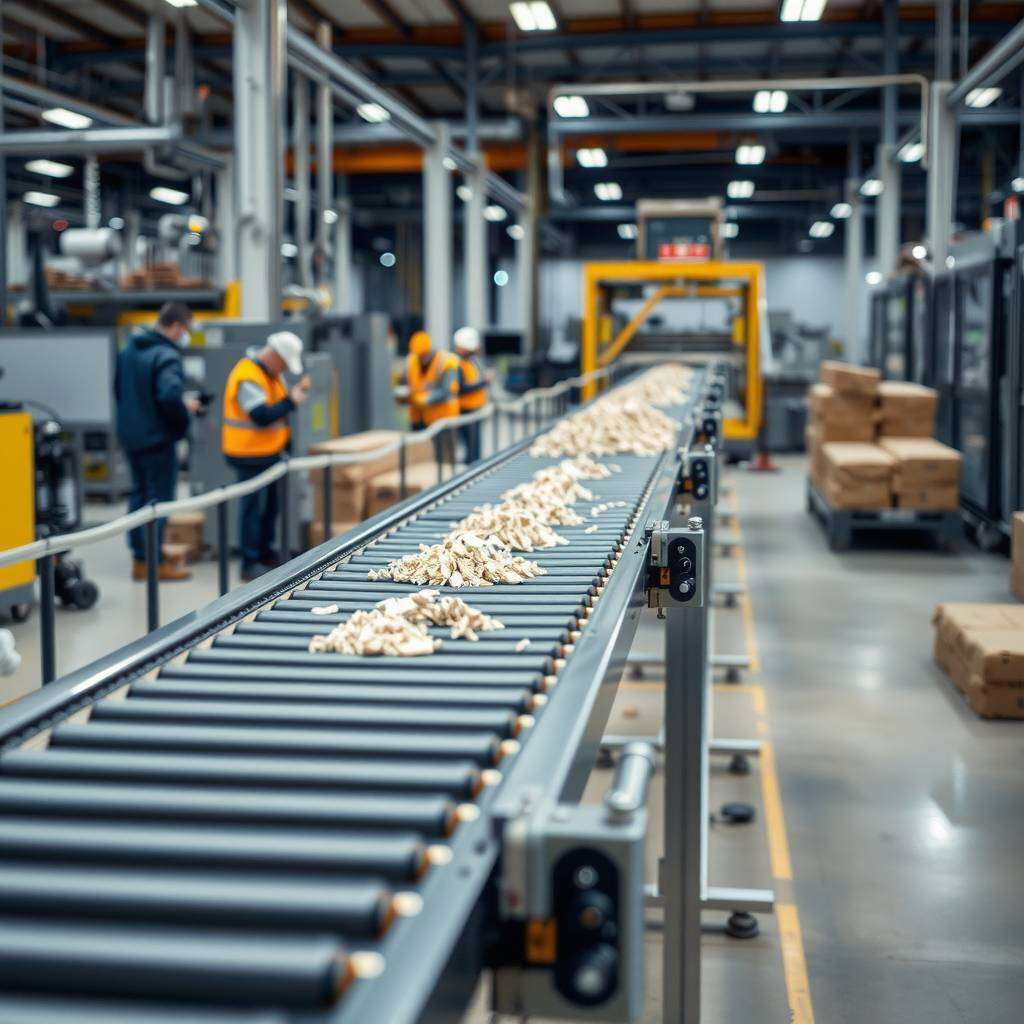
In the fast-paced world of modern industry, efficiency and productivity are paramount. One of the key innovations driving these aspects forward is the conveyor belt conveyor system. These systems have become indispensable in numerous sectors, including manufacturing, logistics, agriculture, and more. By automating the movement of goods and materials, conveyor belt conveyors optimise workflows and streamline operations.
Choosing the right conveyor system can dramatically impact operational efficiency and overall productivity. As a leading belt conveyor manufacturer, understanding the numerous benefits of installing belt conveyor systems for sale can help you make an informed decision that suits your specific industrial needs. Whether you are considering an industrial belt conveyor, agricultural belt conveyors, or flat belt conveyor options, investing in the right system offers substantial advantages.
Increased Efficiency and Productivity
One of the most notable benefits of belt conveyor systems is the significant increase in efficiency they provide. Manual handling of materials can be labour-intensive, time-consuming, and prone to human error. By integrating a conveyor belt into your operations, tasks that previously took considerable time are now streamlined. This automation allows for continuous movement of materials, reducing bottlenecks and ensuring a steady workflow.
For industries dealing with high volumes of materials, such as manufacturing plants or agricultural operations, this efficiency gain can translate directly into increased output and faster turnaround times. As a belt conveyor manufacturer, we see many clients investing in systems like flat belt conveyors or industrial belt conveyors to optimise their production lines and meet customer demand more effectively.
Furthermore, conveyor systems can operate consistently over extended periods, unlike manual labour which might fatigue or slow down. This consistency boosts overall operational throughput, ensuring that productivity levels are maintained at optimum levels.
Versatility and Customisation Options
Conveyor belt conveyors are highly versatile instruments that can be customised to suit specific industrial applications. Whether transferring bulk materials, small components, or fragile goods, there are options available to meet your needs. For instance, a flat belt conveyor is ideal for transporting flat, lightweight items, while other types of belt conveyors may be designed for heavy-duty or irregularly shaped objects.
As a prominent belt conveyor manufacturer, we offer a wide range of belt conveyor systems for sale, tailored to various industries. Agricultural belt conveyors, for example, are built to handle crops or feedstock, with features designed to minimise damage and facilitate swift transfer. Similarly, industrial belt conveyors can be constructed with robust materials for heavy-duty applications, ensuring longevity and durability under demanding conditions.
The ability to modify parameters such as belt width, length, incline angle, and operational speed gives businesses the flexibility to optimise their conveyor system for maximum efficiency. This customisation allows for seamless integration into existing workflows, improving overall operational harmony.
Load Handling and Capacity
Efficiency isn’t just about moving materials quickly; it’s also about handling substantial loads reliably. Belt conveyor systems are capable of carrying large quantities of materials without experiencing significant wear or breakdowns. This capacity makes them indispensable for industries that deal with bulk goods, such as mining, agriculture, and manufacturing.
Depending on the specifications, belt conveyors can handle everything from lightweight cartons to heavy raw materials like coal or ore. Industrial belt conveyors are designed with high-capacity motors and reinforced belts to ensure continuous operation even under strenuous loads. This reliability reduces downtime and maintenance costs, providing a compelling incentive for industries seeking dependable material handling solutions.
Moreover, technological advancements have led to the development of belt conveyor systems with features like variable speed drives and automated controls. These enhancements enable precise load management and optimise flow dynamics, reducing the risk of congestion or spillage.
Improved Safety Measures
Worker safety is a critical consideration in any industrial environment. Manual lifting and handling tasks can expose employees to risks such as strains, knocks, or accidents resulting from falling materials. Implementing belt conveyor systems can markedly improve safety by reducing manual interventions and associated hazards.
Modern belt conveyor systems are equipped with safety features including emergency stop buttons, protective covers, and sensors that detect irregularities or obstructions. These measures help prevent accidents and facilitate swift responses to potential issues.
As a reputable belt conveyor manufacturer, we prioritise safety in our designs. Features such as smooth belt edges, secure fixings, and reliable grounding help minimise risks. Additionally, installing appropriate signage and safety barriers can further create secure operational environments.
Cost-Effectiveness Over Time
Although initial investments in conveyor belt systems, such as industrial belt conveyor or agricultural belt conveyors, may appear substantial, the long-term savings are significant. Reduced labour costs, minimised downtime, and less material wastage contribute to a lower total cost of ownership.
Automation leads to faster processing times and less need for manual labour, which can be particularly beneficial during peak production periods. Furthermore, conveyor systems are generally low-maintenance, especially when constructed from high-quality materials. Properly maintained belt conveyors can operate reliably for years, amortising the initial costs over their lifespan.
Supply options available from leading belt conveyor systems for sale providers include energy-efficient models that reduce operational costs further. As experts in this field, we recommend investing in systems customised for your specific operational requirements to maximise cost savings and operational longevity.
Enhanced Space Utilisation
Optimising space within an industrial setting is vital for operational efficiency. Conveyors allow for better utilisation of available floor space by enabling vertical or inclined transfers. Flat belt conveyor configurations can be designed to fit into tight or constrained environments, while specialised systems can deal with complex layouts.
By precisely routing materials through a conveyor belt system, businesses can free up space previously occupied by manual handling zones, thereby creating more room for other critical operations or storage. In facilities where floor space is limited, installing conveyor systems can lead to better organisation and flow.
A conveyor belt conveyor is essential for efficient material handling in various industries. It streamlines the movement of goods, increasing productivity and safety. For reliable solutions, visit conveyorrollers.co.uk, where you can find high-quality conveyor belt conveyors tailored to your needs. Enhance your operations with trusted conveyor systems from expert suppliers today.
Facilitating Automation and Integration
In modern industry, automation and integration with other systems are crucial for maintaining competitiveness. Belt conveyor systems can be seamlessly integrated with sorting, weighing, inspection, and packaging equipment to form comprehensive automatic production lines.
Automation features such as programmable logic controllers (PLCs) and sensors enable smart operation, including real-time monitoring and adaptive control. This integration enhances overall throughput, consistency, and quality control, reducing the need for human intervention.
By partnering with a trusted belt conveyor manufacturer, companies can access customised systems designed with the latest technological advancements, ensuring your operation stays ahead of industry standards.
Conclusion
Investing in belt conveyor systems offers a multitude of benefits that can transform industrial operations. From improving efficiency and capacity to enhancing safety and space utilisation, conveyor belt conveyors are a proven solution for modern material handling challenges.
Whether you are considering agricultural belt conveyors, flat belt conveyor, or customised industrial belt conveyor systems for sale, partnering with a reputable manufacturer ensures that you get a system that precisely meets your operational needs. Embracing this technology not only boosts productivity but also offers long-term cost savings and operational robustness, positioning your business for sustained success in competitive markets.